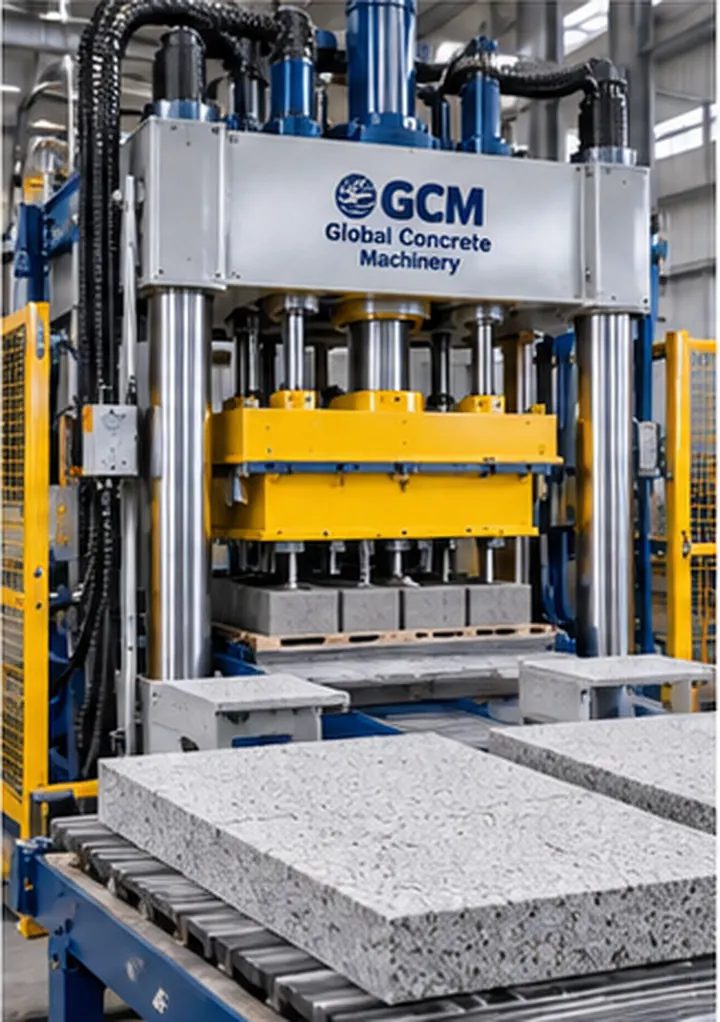

Wet press systems use high hydraulic pressure with wet concrete to manufacture dense concrete products with controlled surfaces and low void content.
Where Wet Press Technology Fits
The process is particularly suitable for kerbstones, paving slabs and selected specialty products where density, surface quality and resistance to water, salt and weathering are important.
Vacuum-Assisted Production
Vacuum removal of excess water can be integrated with high-pressure forming. Product quality depends on concrete recipe, dosing accuracy, pressure, vacuum performance and controlled demoulding.
Plant Engineering
A wet-press line should be planned together with concrete preparation, mould handling, product take-off, palletizing and curing. The press alone does not define plant output.
Project Review
Send target product dimensions, concrete specification and production goals to info@globalconcretemachinery.com for a project review.
Production Scope and Typical Factory Role
Wet Press & Hydraulic Press Systems covers high-pressure forming of dense slabs, kerbstones and specialty architectural concrete products. The category should be evaluated as part of the complete production process, not as a stand-alone purchase. A technically sound project begins with the products that will be sold, the number of shifts, expected production volumes and the condition of local raw materials. Those inputs determine which equipment is essential, which options add real value and which items can be reserved for later expansion. This approach avoids building a factory around a headline capacity that does not match the actual market or product mix.
Define Products Before Equipment
The main selection questions for Wet Press & Hydraulic Press Systems are concrete consistency, pressing force, mould geometry, cycle sequence, vacuum or dewatering, demoulding and curing. Product drawings and expected sales mix should be prepared before final equipment sizing. High-volume standard products and occasional specialty products may justify different tooling, changeover and buffer strategies. Where several configurations are possible, compare them using the same operating assumptions. This makes it easier to see whether a larger machine genuinely creates more saleable output or simply increases capital cost and supporting equipment requirements.
Capacity Must Be Balanced Across the Line
Capacity for Wet Press & Hydraulic Press Systems depends on its connection with material preparation, dosing, hydraulic pressing, mould handling, curing, transfer and optional finishing. The slowest required process determines factory output. Upstream shortages create machine waiting; downstream shortages create pallet congestion, excessive work in process or unplanned stops. During layout review, calculate peak and average flow, identify buffers and confirm how the plant behaves during short interruptions. A balanced line usually delivers better shift output than a system built around one oversized station because operators can maintain a steady rhythm without constantly recovering from accumulation or starvation.
Quality Control for This Equipment Group
Key quality objectives for this category include density, flatness, thickness, surface finish, clean release, edge integrity and dimensional repeatability. Checks should be linked to process variables that can be corrected during production. Approved product drawings, reference samples and recorded recipes provide a stable baseline after maintenance, tooling changes or new raw-material deliveries. Trend data is more valuable than isolated measurements because gradual wear and material drift can be recognized early. When a defect appears, the team should review material condition, equipment condition, settings and handling in a logical order instead of changing several variables at the same time.
Automation and Daily Operation
Daily operation of Wet Press & Hydraulic Press Systems can involve hydraulic cleanliness, mould inspection, seal checks, pressure monitoring, cleaning and safe changeover. Automation should reduce unnecessary manual work and variation while keeping the process understandable to operators. Recipe permissions, alarm history and safe recovery modes should be defined during commissioning. Training should explain why critical limits exist and how one station affects the next. This is especially important in an integrated plant, where a local adjustment can move the bottleneck or create a quality problem several stages later.
Maintenance and Spare-Part Planning
Reliability planning should identify wear items, critical spares and maintenance access before installation. The factory should distinguish daily cleaning and inspection from periodic adjustment and shutdown work. Critical parts should be stocked according to lead time and the production consequence of failure, not simply unit price. Replacement history, recurring alarms and abnormal wear should be recorded. For Wet Press & Hydraulic Press Systems, a maintenance-friendly arrangement improves long-term availability because technicians can isolate, inspect and replace components without dismantling unrelated equipment or blocking the production area.
Factory Layout and Utility Requirements
Final engineering must coordinate Wet Press & Hydraulic Press Systems with foundations, floor loads, clear height, doors, cranes, electrical distribution, compressed air, water, drainage and material logistics as applicable. Service envelopes belong on the layout together with operator and forklift routes. Export projects should also consider shipping dimensions, unloading equipment and installation sequence. Reserving sensible expansion space is usually inexpensive during initial construction and very expensive after permanent structures or utilities have been placed in the only practical growth area.
Investment and Expansion Strategy
The investment case should include press capacity, mould count, hydraulic maintenance, labour, curing, finishing and product selling value. Purchase price is only one part of the decision. Labour, consumables, maintenance, rejects, energy and downtime can change the economics significantly over several years. The highest automation level is not always the best starting point, and the lowest initial cost may restrict growth. Compare a realistic base-demand case with an expected-growth case, then identify which upgrades can be added later without replacing major equipment. This creates a clearer path from initial production to a mature factory.
Questions to Resolve for Wet Press & Hydraulic Press Systems
Before this machinery group is released for final engineering, the customer and supplier should agree the product drawings, target volumes, operating hours and the assumptions behind concrete consistency, pressing force, mould geometry, cycle sequence, vacuum or dewatering, demoulding and curing. The discussion should also cover how material preparation, dosing, hydraulic pressing, mould handling, curing, transfer and optional finishing will be supplied, controlled and maintained under normal plant conditions. If the factory expects a wide product range, identify which changes require tooling, recipe changes, extra cleaning or additional handling. If expansion is expected, define which interfaces and building areas must remain available. These decisions give the category a clear role in the factory and prevent optional equipment from being selected without a specific production reason.