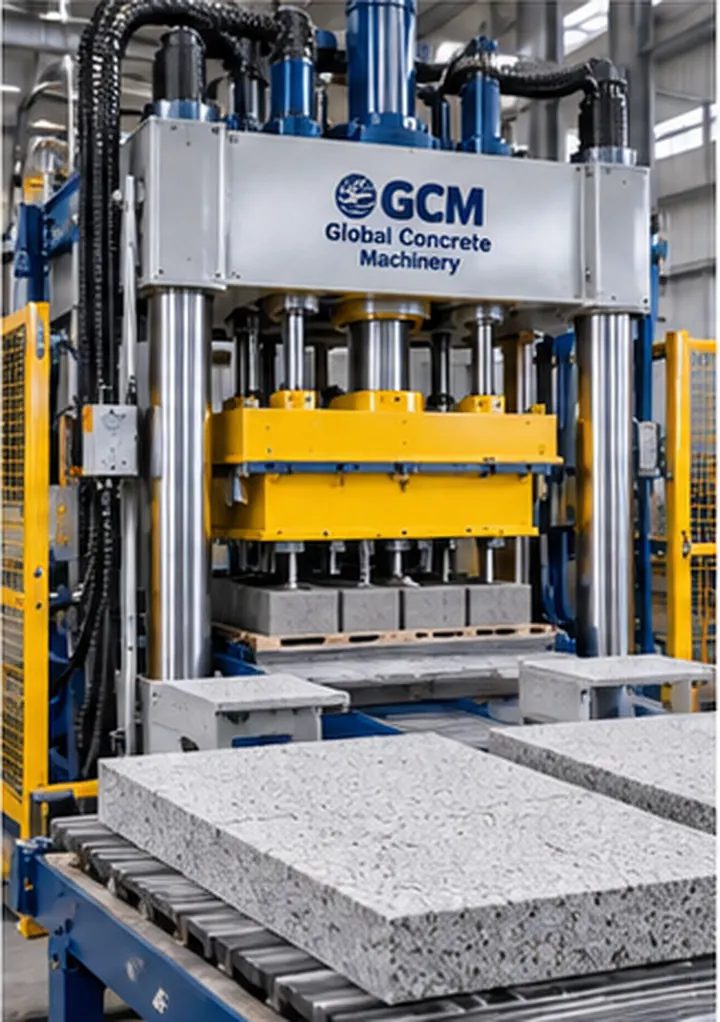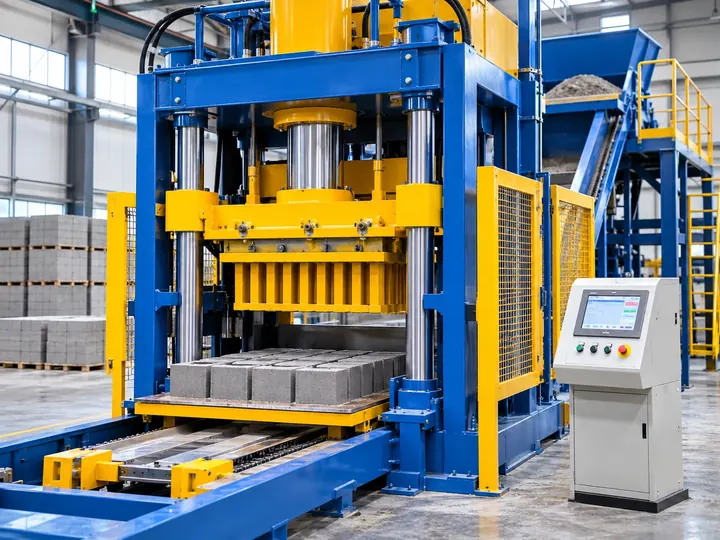

GCM M1200 Mobile Block & Kerbstone Machine
Mobile egg-layer style concrete-products machine for direct-floor production of blocks and kerbstones without a conventional pallet circulation system.
Technical Specifications
| 20 × 40 × 20 cm block capacity | 10,000–12,000 pcs / 8 hours |
|---|---|
| Kerbstone capacity | 3,000–4,500 pcs / 8 hours |
| Hydraulic power | 35 kW |
| Press area | 1250 × 850 mm |
| Working pressure | 160–180 bar |
| Reference product height | 200–500 mm |
In the context of GCM M1200 Mobile Block & Kerbstone Machine, Capacity figures are reference values for the stated product and shift period. Actual production changes with mould design, concrete recipe, product geometry, operator settings, curing and the balance of the complete production line.
Typical Products
- Concrete blocks
- Kerbstones
- Direct-floor production layouts
- Projects where pallet circulation is intentionally avoided
Production-Line Integration
A mobile machine changes the plant layout because fresh products remain on the production floor while the machine advances. Floor quality, curing organization, forklift routes and weather protection therefore become key project variables.
Project Configuration
In the context of GCM M1200 Mobile Block & Kerbstone Machine, before quotation, Global Concrete Machinery reviews the required products, mould drawings, target shift output, factory dimensions, curing method, automation level, electrical standard and destination country. This allows the forming machine and the surrounding batching, handling and packaging equipment to be sized as one production system.
Concrete Feed, Vibration and Compaction — GCM M1200 Mobile Block & Kerbstone Machine
GCM M1200 Mobile Block & Kerbstone Machine should be configured for tall or heavy kerbstone profiles that need reliable mould filling and handling. The first engineering step is to define product geometry, mould cavity layout, pallet format, concrete consistency, vibration settings, pressing sequence and target cycle. These values determine whether the equipment will work comfortably inside the intended production window or will constantly need corrective adjustment. Settings should be established with the actual raw materials, product geometry and tooling that will be used in production. A machine that is stable at a realistic operating point usually delivers more saleable output over a shift than a machine pushed to a theoretical maximum that causes frequent stops, rejects or excessive wear.
Mould and Pallet Compatibility — GCM M1200 Mobile Block & Kerbstone Machine
The main process objective for GCM M1200 Mobile Block & Kerbstone Machine is uniform cavity filling, stable green strength, consistent density, dimensional accuracy, clean edges and repeatable surface appearance. That requires the machine and its tooling to work as one system. Product dimensions, contact surfaces, alignment and material condition should be checked during setup and after defined production intervals. When a visible defect appears, the team should avoid changing several settings at once. A disciplined sequence—material condition, tooling condition, machine alignment, process settings and handling—makes the root cause easier to find and prevents temporary adjustments from hiding a mechanical or material problem.
Balancing the Machine With the Line — GCM M1200 Mobile Block & Kerbstone Machine
GCM M1200 Mobile Block & Kerbstone Machine does not create factory capacity by itself. It must remain synchronized with batching and mixing, product feeding, pallet circulation, wet-side transfer, curing, dry-side handling and cubing. Each interface needs enough capacity for normal production and a sensible response to short stoppages. Buffering can help, but excessive buffers increase pallet inventory, floor area and work in process. During layout review, follow the material and product path from receiving to dispatch and confirm transfer heights, maintenance zones, lifting access, safe walking routes and forklift movement. This process-flow check often identifies practical restrictions that are not visible in an isolated machine datasheet.
Quality Signals During Production — GCM M1200 Mobile Block & Kerbstone Machine
Operators should monitor signs that show whether GCM M1200 Mobile Block & Kerbstone Machine is running consistently: cycle behaviour, product appearance, abnormal noise, temperature, vibration, hydraulic response, transfer timing and recurring alarms as relevant to the equipment. Quality staff should connect these observations with measured product results. Trend data is more useful than isolated readings because gradual wear or material drift can be detected before it creates a large batch of nonconforming product. Approved reference samples and documented machine settings are especially useful after mould changes, maintenance work or the introduction of a new recipe.
Maintenance Points That Protect Availability — GCM M1200 Mobile Block & Kerbstone Machine
Planned maintenance for GCM M1200 Mobile Block & Kerbstone Machine should cover mould and tamper wear, vibration elements, hydraulic units, guides, sensors, pallet condition, lubrication and frame fasteners. The maintenance plan should distinguish daily cleaning and visual checks from weekly inspection, periodic adjustment and planned shutdown work. Wear limits are better than waiting for failure. Critical spare parts should be selected according to lead time and the consequence of a failure, while replacement history should be recorded so recurring problems become visible. Service access should be considered in the factory layout, because a component that can be reached safely and quickly is far less expensive to maintain over the life of the line.
Automation and Operator Control — GCM M1200 Mobile Block & Kerbstone Machine
Automation should make GCM M1200 Mobile Block & Kerbstone Machine more repeatable without making the process opaque to the production team. Recipe control, interlocks, alarms, counters and automatic sequences should have clear ownership and backup procedures. Operators need to understand what the machine is trying to achieve, what conditions must be present before a cycle can continue and how to recover safely from normal faults. Supervisor permissions can protect critical parameters from accidental changes, while maintenance modes should support diagnostics without bypassing safety. Good training covers abnormal conditions and shift handover, not only normal start and stop procedures.
Installation and Utility Planning — GCM M1200 Mobile Block & Kerbstone Machine
Before the final configuration of GCM M1200 Mobile Block & Kerbstone Machine, confirm the available electrical supply, floor and foundation conditions, clear height, doors, lifting equipment, water or compressed air where required, ambient conditions and the planned installation sequence. The customer and supplier should also agree which connections belong to the machine scope and which belong to the site contractor. Drawings should show operating space and maintenance space. For export projects, transport dimensions, packing, unloading equipment and the order in which equipment reaches the building can affect commissioning just as much as the machine specification.
Where This Machine Fits Commercially — GCM M1200 Mobile Block & Kerbstone Machine
The commercial evaluation of GCM M1200 Mobile Block & Kerbstone Machine should include mould investment, pallets, labour, energy, wear parts, reject rate, maintenance time and the value of future automation. A lower purchase price can be offset by additional labour, frequent stoppages, high consumable use or short wear life. The highest automation level is not automatically the most economical either; it should match expected sales volume, labour conditions and maintenance capability. Compare at least a base-demand case and a growth case, then identify which future upgrades can be added without replacing major equipment. This approach produces a clearer investment decision and keeps the factory aligned with the products it can realistically sell.